Circularity does not begin in the reconditioning workshop, but in the returns logistics. After all, without a well-organised return flow of used parts, there is nothing to recondition. At DAF, this return chain has formed the basis of PACCAR Parts’ remanufacturing programme for over fifty years, processing hundreds of thousands of parts annually.
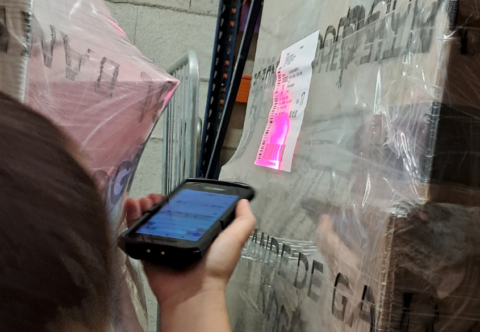
“The first step towards circularity isn’t remanufacturing,” says Remanufacturing Programme Manager Teun Dingen. “You first need to ensure that parts actually come back to you in the first place.” That sounds obvious, but in practice it requires a carefully organised process. For example, as soon as a dealer replaces a turbocharger, starter motor or gearbox, the old part is registered. On the next delivery run, DAF collects the faulty part straight away. This marks the start of a second logistics chain, running alongside the regular distribution of new parts.
SLF themes
Although Dingen itself has no direct involvement with the Service Logistics Forum, the subject of remanufacturing ties in seamlessly with the themes around which the SLF has been bringing together companies, researchers and knowledge institutions for thirty years: reverse logistics, extending the service life of parts and the organisation of circular service chains. PACCAR Parts Europe has therefore been involved with the SLF for many years.
Deposit
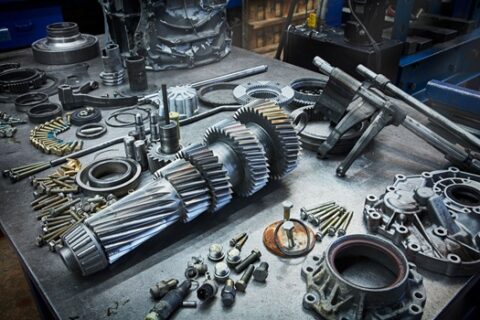
PACCAR Parts uses a deposit-refund scheme to encourage dealers to return parts. Dealers pay a deposit when purchasing a part and have it refunded as soon as the old part is returned within the specified timeframe and in satisfactory condition. “That’s the incentive to actually return parts,” explains Dingen. “But just as important is that we make returning parts as easy as possible. If a customer has to go to a lot of trouble or incur extra costs to return parts, the system won’t work.” This approach has proved effective. Every year, PACCAR Parts receives around 450,000 parts in return. This provides the company with a virtually continuous stream of used parts that serve as the basis for reconditioning or recycling.
More than just a repair
A common misconception is that remanufacturing is the same as repairing. According to Dingen, there is in fact a fundamental difference. “With a repair, you only replace the faulty part. With remanufacturing, you repair or replace the faulty part and carry out a full inspection of the entire product. We test all parts against the same technical specifications as a new product. If a part does not meet these specifications, it is replaced. Ultimately, the remanufactured product must offer the same quality and the same warranty as a new part.” It is precisely this quality guarantee that makes the remanufacturing programme attractive to the end customer: the hauliers. They receive a part that is technically equivalent to a new one, but at a lower cost. According to Dingen, as soon as a remanufactured variant becomes available, customers almost always switch to it.
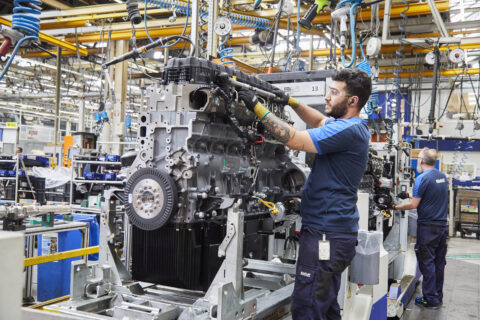
DAF Eindhoven Plant
Logistics challenge
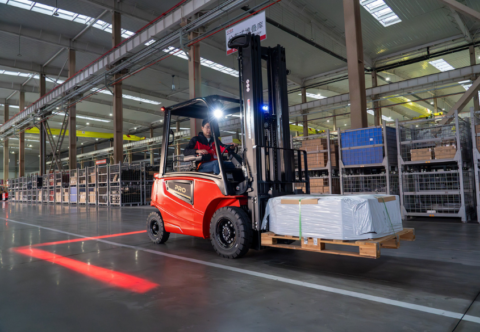
Behind the scenes, remanufacturing proves to be primarily a logistical challenge. Upon receipt of returned parts, all components are inspected, processed administratively and stored temporarily. They are then sent to an in-house reconditioning workshop or to specialist reconditioning partners. Only after complete disassembly, inspection, replacement of worn parts, reassembly and extensive final testing do they return to the warehouse to be delivered to dealers once more. “Recovering parts is actually just the start of a new cycle,” says Dingen. “After that, the whole process begins again.” This requires a dedicated logistics organisation. In the so-called Core Warehouse alone, several dozen staff members are busy every day receiving, checking, registering and distributing the return flows.
Business case
Although sustainability now plays a key role in PACCAR Parts’ strategy, remanufacturing was never driven solely by environmental considerations. The programme has been in place for over fifty years and was originally developed primarily because it made good business sense. That remains the case today. Before a part is added to the remanufacturing programme, PACCAR Parts assesses it on the basis of three questions: is it technically feasible, is there a sound business case, and is there sufficient market demand? “If remanufacturing becomes more expensive than producing a new part, it stops,” says Dingen. “Legislation and regulations certainly provide us with an extra incentive, but ultimately a programme must be able to support itself financially.” It is this combination of sustainability and economic logic that, in his view, makes remanufacturing so powerful.
New technology, new opportunities
Meanwhile, the reconditioning programme is constantly evolving. Whereas in the past it was mainly mechanical components that were reconditioned, the focus is increasingly shifting towards electronic components. Printed circuit boards and electronic control units offer great opportunities, although it is technically more complex to demonstrate that a remanufactured part has the same reliability as a new one. According to Dingen, the rise of electric lorries will also further increase the importance of remanufacturing. Although electric vehicles contain fewer moving parts, the components are often considerably more expensive. “That is precisely what creates an interesting business case. If such an expensive component can be remanufactured, it delivers significant value for both the customer and the manufacturer.”
According to Dingen, the underlying principle is more widely applicable than just to the lorry industry. Machine builders, manufacturers of industrial plant and suppliers of agricultural machinery can also set up similar systems, provided there is a sufficient supply of spare parts in circulation and a sound business case exists. “If you want to operate in a circular way, don’t start with reconditioning. Start with a good returns strategy. Without a reliable flow of used parts, you cannot build a circular system.”
Text: Pieter Pulleman